Saturday, March 26, 2011

Lyman 358-477 : 150 grain SWC: Accuracy Results

Accurate results with the lighter bullets has been impossible, so far. Today with a medium crimp and  loaded over 3.5 grains of 700X, success!   A very accurate sub-1-inch 5 shot group of .69.  That makes the 358-477 one of the best moulds for the 357 Magnum revolver.  The actual bullet looks different than Lyman's website:


As always, that's with a Taurus 66, 6 inch barrel, from at rest at 25 yards.  The Taurus is now carrying a Simmons 4X scope which is very effective.  Here's a picture, the 358-477 group is the first target:


The updated details of the load are in the Most Accurate Bullet Moulds and Loads Table

Additional tests are planned to further refine the OAL, which is very important for this bullet.  I will be testing magnum powder charges in the future, but the initial results are not worth mentioning so far.  That may change, and the results will speak for themselves.

The 358-477 works great loaded long, tested with a OAL of 1.620 (a little shorter may work) and lubed with Darr lube. 

FYI:  NRA lube is quickly becoming my favorite, and works well with all 357 bullets, including this one.  The high quality and the low price of the hollow sticks from White Label Bullet Lube make it a great value.  NRA has been a favorite for cast bullet shooters for years, and with good reason.

The 358-477 is super accurate, with light recoil and very economical to shoot.  The Lyman steel/lead moulds cast great and won't break the bank.  Available new in 2 cavity and 4 cavity versions and available from all the web-sites that sell resloading / casting equipment.  Midsouth has the best price right now, at least that I can find.

Sunday, March 20, 2011

357 Magnum Cast Bullet Crimping

A short note on the roll crimp used for cast bullets:  Nothing in casting and handloading works for everyone, for all guns, for all reloading presses and in all instances.  Crimping is just like that.  You will have to adjust a bit, but crimping does affect accuracy and is important.

I do know the Lee crimping dies and the Dillon Square Deal B dies do work with these adjustment specs (note: the Lee FCD can cause problems. For accurate cast bullets that are oversize at .360 diameter, a regular roll crimp die works best.): 

Crimping cast boolits without a groove, or crimping on the driving band:  This takes pure experimentation.  The Lyman 358-429 crimped onto the front band works well with a light roll crimp.  It's important to crimp enough so the bullets don't jump out of the case due to recoil, and not to much crimp or it will ruin accuracy.

The 700X and HP38 loads in the Most Accurate Boolits and Loads Chart have a medium crimp.  The 700X 5.1 load and all the H110 & 2400 magnum loads have a heavy crimp.

What does this mean?  First, here's how I zero the crimp:

  1. Back out the crimp die
  2. Size a fires 357 magnum case
  3. Place the case under the crimp die and raise the ram (don't use a flared case)
  4. There should be no contact between the crimp die and the mouth of the case
  5. Holding the ram up, Screw in the crimp die until it make firm contact
  6. Now the crimp is  zeroed
Once you are at this point, lower the ram and screw in the crimp die to the crimp needed:
  • Light crimp = 1/2 additional turn of the crimp die from zero
  • Medium crimp = 3/4 additional turn of the crimp die from zero
  • Heavy crimp = 1 additional turn of the crimp die from zero
This isn't how everyone does it, so this terminology isn't universal.  Most all non-magnum loads work well with a medium crimp.  The magnums and the non-magnum powder- near-max-pressure loads work with a heavy crimp.  For example, 5.1 grains of 700X works best with a heavy crimp.

Bullet diameter plays an important factor with the crimp setting.  Recently, with full size .360 diameter bullets, and using a Lee seating/crimp die, a light crimp proved to work the best.  

The 148 wadcutters also work well with a medium crimp.  I've not been able to produce good results with a light crimp on a wadcutter as many recipes or tips advise.  It's worth a try if you are shooting a full wadcutter.  Like the opening said; nothing in casting and handloading works all the time.

Wednesday, March 9, 2011

Initial test results: Casting at 725 VS 925 degrees. How bad is casting hot????

So this topic has been bothering be for some time.  I've often heard concerns of what happens to WW and other bullet alloy when casting with a hot pot.  So it was time to run a test.  I also wanted to figure out how to soften WW to meet my needs in my 357 magnums.

Added for clarification:  There is a popular idea that casting with a hot pot cooks out the tin and antimony from the WW alloy.  If that happened the alloy would be softer.  Their follow on argument is that a hot pot oxidizes out the tin and antimony, some cliam within minutes. Again, if either point is true, the alloy will become softer. 

Added:  How to harden and soften cast bullets using heat is an upcoming topic.  However a few other projects are first.  A much closer look at H110 in the 357 Magnum is not-to-far-off.

I figured I'd cast test bullets at intervals (see below) and measure the BHN after 1 day, 7 days and 14 days.  After 1 day I'm shocked enough to post the first results.

The test scenario is straightforward:

The 725 degree test and then the 925 degree test are identical:
  1. Clean out the pot
  2. Put in 3 lbs of WW
  3. Bring the lead to 725 or 925
  4. Cast 4 bullets - minute 0 of the test
  5. Cast 4 bullets - at the 30 minute mark
  6. Cast 4 bullets - at the 60 minute mark
  7. Cast 4 bullets - at the 120 minute mark

725 BHN results after 1 day:
    0 min = 10.4
  30 min = 10.4
  60 min = 10.4
120 min = 10.4

925 BHN results after 1 day:
    0 min = 10.4
  30 min = 10.4
  60 min = 10.4
120 min = 10.4


There is no negative impact on BHN from casting with a hot pot. 


My goal of wanting to cook WW down to a softer BHN isn't going to work out.  I'll wait a week and see if results change at all.  But I didn't expect them to be 10.4 this quickly and don't foresee them getting much harder, if at all.

The next time someone tells you the horrors of casting with a hot pot and the major impact of oxidizing tin etc... and having a major negative impact on the bullets, you don't have to take their word for it.  You don't have to take my work for it either. The test is easy, try it yourself and see what your results are.

I plan to continue casting hot as I find it to work well.  Now that I know for a fact there's no negative impact on the alloy, there's no reason to be concerned at all.

Update:  Here is a snippet from the  Lyman Cast Bullet Handbook, third edition, page 43.  The tin and antimony doesn't cook out of the lead.  It's apparently difficult to remove enough tin / antimony to matter. Cooking 2 hours at 925 oxidized out some tin possibly, but it still measured 10.4 BHN, it made ZERO difference.


Saturday, March 5, 2011

Accuracy Results: Lyman 357-446 & Lyman 358-429

The older Lyman 357-446 mould is found on eBay and other web auction sites these days.  They is an great buy.  Test results at 25 yards are excellent with the potential of groups less than 1 inch.  The best group being .78 inches.

UPDATE on 3/19/11: The Lyman 358-429 seated at 1.620, crimped into the front driving band works great. It shot a best group of .8 inch over 11.8 grains of H110 at the range today.  That was out of 3 groups of 5.  It liked a light crimp, but more testing is needed to confirm the bullets don't pull out a bit under heavy recoil.  I'll add it to the next version of the Accuracy Chart.

UPDATE on 4/23/11: Note, I ran across a few Lyman moulds that drop undersized bullets.  This can really impact accuracy.  Just a warning to measure the bullets, and have Lyman fix any problems that exist.


The Lyman 358-429 is available new from any of the online shooting supply sites.  Midsouthshootersupply.com has the best prices right now, that is always subject to change.

If you are a new reader, all tests are conducted at 25 yards, off a rest.  This time a Simmons scope has replaced the Red Dot.  With a 1 inch "dot" in the Red Dot,  it makes testing difficult.  Hiding 1 inch is a bunch when attempting to shoot 1 inch and smaller groups.  I'm still getting used to the Simmons, but like it quite a bit.  Oh, its a 4X power scope too, works out great at 15 yards too.

The 357-446 is an older discontinued design and has some controversy surrounding it.  You decide if it matters to you, it doesn't to me and I plan to keep it.  Some reports claim this bullet starts having flyers at 50 yards, and the problem gets worse at 100 yards.  Specifically at 38 special velocities, which the super accurate load below is.  This is a good shooting and good looking bullet design.


If you shoot at very long distances at 38 special velocities it may make a difference to you.  If not, this is a great mould that is readily available on eBay, and other auction sites.

This is now ranked fourth on the Most Accurate Boolits and Loads chart:


RankMouldWeightGroupChargeOALVelocity
1360-200-SWC2000.573.4, 700X1.614660
2358-429 NOE1680.584.7, HP-381.620900
2358-429 NOE1680.585.1, 700X1.6201,200
3158-SWC TL1580.613.5, HP-381.600810
4357-4461620.783.5, 700XGroove890
5358-429 NOE1681.0011.8, H1101.6201,260
6158-SWC TL1581.105.1 HP-381.6001,129
6148-WC TL1481.103.5 HP-381.400928
7360-200-SWC2001.183.0, 700X1.614660
8360-145-SWC1451.203.9 700XGroove1,020
9358-429 NOE1681.3010.3,24001.620910
10140-FN-LBT1401.405.8 700XGroove1,347

The alloy used id the proven soft mix or lead/solder at 50/1 .

The Tarus 66 has a .357 groove diameter with .358 cylinder throat sizes.  This is optimum, not all guns are this cast-boolit friendly.  That means they produce bigger groups.  I'll stick with the Taurus and the small groups.

Saturday, February 26, 2011

Extensive Mould Temperature Test & Results – Finding the Mould Temperature Sweet Spot

What is the optimum mould temperature to produce the best bullets possible?  After testing temps of alloys and how it affected bullet diameter, folks wanted even more test results, this time focusing on the mould itself.  Here it is!

The first challenge and what prevented me from doing this before is the problem of accurately measuring mould temperature.  The answer is the NOE Digital Casting Thermometer.  It attaches to the mould by inserting the probe into the mould, once drilled using the supplied drill bit.  There are instructions on where to place it on NOE moulds.  It’s easy enough to determine positioning on other brand moulds too.   

This is the unit and its components:


Here’s how it looks inserted into the mould:


Positioning the unit properly while casting keeps the wire out of the way and made it very easy to use.  It worked well with my casting process which is:
  1. I cast with the pot to the left (this is to give you an idea how it worked)
  2. Let the sprue firm up and “suck” itself in
  3. Flip the mould and with a whacker drop the sprue into a container one step to the right
  4. Sprue side down and with the mould held close to a drop cloth, drop the bullets
With this process, moving from left to right, the digital unit works well position just to the right of the drop cloth, at drop cloth level.  It keeps the wire out of the way and makes for a quick temperature check after dropping the bullets.  Very nice!

Note, this an important point: the test results must be adapted to be effective during a casting session.  I've also notice a variaton between different thermometers, so your best temps should verified and adjusted if needed.  

Also, all testing and results is with 98% lead and 2% solder.  This alloy likes things a bit hotter than harder alloys, such as wheel weights.

When preheating the mould (hot plate or dipping into the alloy) the cavity temperature is a bit cooler than the mould block itself.  The temps in the charts during the test are mould block temps, the cavity is a little cooler.  I decided to be consistent and report what the actual mould temps are during testing.  I will explain how to adapt for a casting session in just a minute
.
First, the test process for my test mould (358-429 aluminum 5 cavity from NOE);

Preheat the mould to the desired test temperate by heating it on a hotplate.  As the temps increased it had to be  dipped  it into the alloy for the hotter tests.

The results are in following three separate charts:
  1. Bullet diameter measured on the casting seam
  2. Bullet diameter measured 90 degrees across the seam (cross)
  3. The difference between the two diameters or the amount the bullet is out of round
The diameters measured on the seam (big is best):


The diameters measured across the seam (big is best):


The amount “out of round” (small is best):


Click on any picture or image to see a larger full size version.


The best bullets, the biggest and most round, result from a mould preheated to 440 degrees.  Hotter than that and the roundness and overall size falls off quickly.  

The window for the absolute best result is very narrow.  That can be a challenge.  Maintaining the optimum temp by feel and experience is good, but not the best solution.  I now use the Digital Casting Thermometer all the time, because it works well.  It's all about great results.

Now, how does this work in a real casting session.  It turns out that while casting, the heat is now coming from the cavity instead of outside the cavity.  The cavity and mould temp are now much closer to each other.

With that in mind, keep the mould between 410 and 420 to produce absolutely terrific bullets.  They are very round, as good as the best test results, full sized too.  Some early signs of frosting may show, without impacting bullet quality at all.

The actual in-cavity temperature is 420 degrees as well.  Verify it with a kitchen flat bottom thermometer to get started, if that's what you have on hand.  The Digital Casting Thermometer makes getting started and then maintaining the optimum temperature a breeze.

Added:  Lyman steel moulds work well preheated to 380 degrees, using the kitchen thermometer insterted into a cavity.
 
Heating the mould hotter than 420 degrees produces frosted bullets and the results are not as round and are not fully sized.
 
I found it was hard to keep the mould up to 420 degrees, luckily it didn’t need to be hotter.  At 520 degrees the squared grooves in the bullet design make it a bit tricky to get them to drop, but a couple of taps shakes them loose.  

The best solution proved to be; preheat to 420-430, using the Digital Casting Thermometer from NOE, and then pace the casting so the mould temp maintains 410-420 degrees.  The bullets and mould are into their “sticky” area at these temps, backing down a bit to 400-415 may help and won’t hurt the results.

Adjusting my process based on these test results, and using the thermometer has improved my casting and the bullets I produce. Pacing the casting process to maintain the perfect temperature works best.  Using a wet cloth to cool the mould was rarely needed, but with the thermometer all guessing and estimating is removed.  Speed up to get more heat and touch the mould to the damp cloth when it gets over heated.

Now I know the perfect temperature for a 358-429 aluminum mould.  I will also test others to verify their best casting tempurature, or to know their “temperature sweet spot”.  In any case, knowing the perfect mould temp produces better quality bullets, because they are fully sized and more consistent than ever.  

This translates to improved accuracy at the range.

Friday, February 18, 2011

357 Magnum Accuracy is About Semi-Wadcutters. Overview of Most Accurate Moulds.

Review the most accurate load chart just below, and it's glaring that semi-wadcutters (SWC) are at the top.  (Note the 358-429 is a Keith and a SWC.)  Testing has included round nose, flat nose and wadcutter designs as well.  Calling out moulds that aren't the most accurate isn't the goal here, so there won't be a long list of what hasn't worked very well.  But, there are many.

This is the current accurate load chart, it will we updated and posted to a page of it's own sometime soon: (click the Most Accurate Bullet Moulds and Loads Table at the top of the right frame for the latest load data, Also see the latest favorite mould list at Lyman 358-477 Added to Favorite Bullet Moulds and Loads.  Also look at a custom 358-429 from Mountain Molds)
RankMouldWeightGroupChargeOALVelocity
1360-200-SWC2000.573.4, 700XGroove660
2358-4291680.584.7, HP-381.620900
2358-4291680.585.1, 700X1.6201,200
3158-SWC TL1580.613.5 HP-381.600810
4358-4291681.0011.8, H1101.6201,260
5158-SWC TL1581.105.1 HP-381.6001,129
5148-WC TL1481.103.5 HP-381.400928
6360-145-SWC1451.203.9 700XGroove1,020
7358-4291681.3010.3,24001.620910
8140-FN-LBT1401.405.8 700XGroove1,347

Absence from the most accurate list means; they aren't that accurate or haven't been tested yet.  Not when shot from a rest at 25 yards, and multiple 5 shot groups measured with calipers.  Anyone can claim they shot off-hand (two handed & unsupported grip) and the gun shot better than they could, with any bullet.  Of course it does.  Remove the shooter from the equation as much as is afford-ably possible and run multiple tests, measure the groups with calipers and sort them.  That's the only way to correctly determine which moulds and bullet designs are the most accurate. 

The list I maintain is the very top of the tested-measured-sorted list, the most accurate cast bullets for your 357 magnum.

Various "max bullet in the chamber" designs as well as the standard flat nose, and various wadcutters have all been through the wringer.  There may be a few new designs that test well, but they would be big shock at this point.

Two big surprises are:
  1. Wadcutters aren't as accurate as SWC's
  2. Lighter bullets such as the 140, 145 and some 150 grain versions don't do all that well.  These are usually touted as the most accurate of all 357 bullets, but haven't proven it
  3. The Lyman 358-477 design at 150 grains is an exception and groups less than 1 inch
Two big learning points are:
  1. SWC's ranging from 158 grains to 200 grains are generally the most accurate, those and the Lyman 477 comprise 100% of the groups less than 1 inch
  2. Keith style/design bullets do very well, but note that other SWC's are also on the list too, see pictures below
Note: It's really the length of the bullets that is important, longer bullets weight more which is why the weight and length are related.  The length / diameter ratio has a lot to do with the accuracy.  While this isn't the only factor about bullet design that is important, it is one important and often overlooked factor.

Looking at the results, it's obvious that longer bullets are more accurate.  Also, a SWC is typically longer than a  flat-nose of the same weight.  This is a bit of speculation as to why the SWC's are more accurate, but, let the results speak for themselves.  Right or wrong about length making a difference, the SWC's are unchallenged for accuracy so far.

The three bullets below from left to right are:  360-200-SWC (200 grain SWC from a NOE mould), 358-429 (168 grain Keith is from a NOE mould, it has a shorter nose than the Lyman and may fit your gun better.  The longer Lyman design won't work in every 357, you have to test any 358-429 in your revolver or crimp it into the front driving band).  These are the top 2 accurate bullets I load and shoot.  The third bullet in the picture is from an very old Lyman 357-446 mould that drops a 162 grain SWC.  It's undergoing testing now.  Some others have reported excellent accuracy, others reported accuracy issues.  It's interesting to look closely at the three, as they are all very similar:


Here's a closer look at the 200 SWC, the best group I've every shot are with this bullet (by .01 inch):


A closer look that the 358-429 168 grain Keith which is also super accurate, and virtually in a tie with the 200 SWC.  Just .01 inch at 25 yards separates them, and that  is splitting hairs:


The other mould that groups less than 1 inch at 25 yards is a Lee 358-158-TL, which I don't have a photo of.  Here is the drawing from the Lee site.  It's very similar to the other SWC's except for the lube grooves.  If you don't mind tumble lubing, many folks like how easy it is, this is incredibly accurate and very inexpensive.  A six cavity mould creates a large pile of bullets quickly too.


The current mould/bullet in test is the old Lyman 357446, here's a closer look the bullet it produces:


All the pictures expand when you click on them.  Take a close look.  I really like the big squared lube groove of a Keith style SWC.  However the Lee is very different and is incredibly accurate as well.

If you are striving for the most accurate bullet/load in your 357 magnum a SWC from 158 to 200 grains is for you.  If you can buy these particular moulds, they are proven (pending results of the 446).  If you have one that looks very similar, you can use the "most accurate loads" and be close.  Then work up the perfect load for your revolver.  The specific design of the 358-477 is also a proven accurate bullet too.  Other designs in this size/weight haven't worked as well.

The Accurate Load chart will be updated soon.  It was to include early results with a new-to-me Dan Wesson with a 6 inch barrel.  The groove size of the Taurus is .357 while the Dan Wesson is a huge .3588.  The DW isn't liking the stiffer charges with fast powder.  The Taurus 66 6 inch has proven to be more accurate than any other 357 revolver I've shot.  Mine has .358 throats and at .357 groove, perfect for cast shooting.  Some other makes have optimized for jacketed to the point of affecting accuracy of cast bullets.

If you are in the market and want a very accurate 357, consider getting a long barrel Taurus.  Forget what everyone says about the other brands being better guns.  Get the Taurus and out-shoot them.

Just for fun here's a handful of the 168 grain Keith's, including the nasty looking one with the rounded base:

Saturday, February 12, 2011

Final report on the changing bullet diameter, sized and unsized. How to use it to improve accuracy.

The soft alloy that is so accurate in a 357 magnum drops from the mould a little smaller than harder alloys.  Having the optimum alloy is more important than the optimum size, so the soft alloy is the best approach.  You can then use the changing size to squeeze the last bit of accuracy out of the bullet.  Read on:

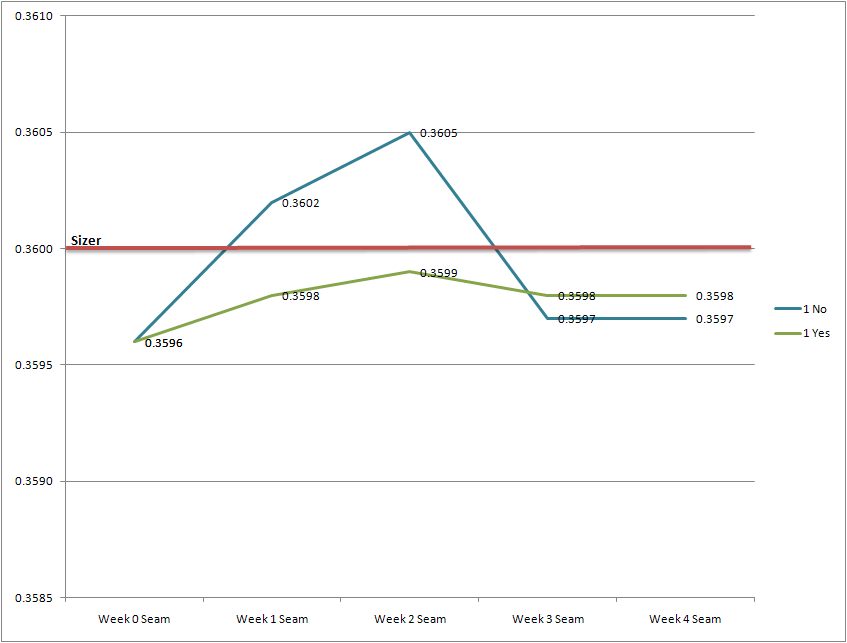
The final measurements of this test are in the chart below.  The blue is not lubed, the green is a lubed bullet.  Note the sizer line at .360 inch.  That's the actual measurement that my Lyman 450 sizes at.  Check yours as they can be vary a bit:


Click on the graph for a full size readable view.

In case you haven't had a chance to read the prior post, the blue line is a bullet that was unsized/unlubed measured on the seam for 4 weeks.  The green line is a bullet from the same cavity, cast a few seconds later.  It dropped at the same exact size, as you would expect.   Shortly afterwards the second bullet was put through a Lyman 450 Lubrisizer.  The sizing .360 die (the highlighted line) didn't change the size at all since the bullet was smaller.  FYI, the lube is Darr Lube, which is my go-to homemade lube.

The results are striking.  The lubed bullet stayed close to the same size, expanding a little bit and then constant.  The unlubed bullet grew above the .360 size, which works best for accuracy and is very useful.  What's also useful is the fact that once lubed the bullets stay fairly even over time.

Recognize that not every bullet grows the exact same amount.  Also recognize that a bullet doesn't expand/grow the same amount evenly.  The ideal process to use this new information is:
  1. Cast the bullets
    1. The 50/1 lead/solder alloy likes 900-975 degrees
    2. It also likes the mould preheated to 400 and kept between that and 420 (cavity temps).  There will be more extensive cavity temp test results coming as even hotter mould temps may offer some advantage.
    3. This is considered too hot by many, it isn't for this alloy.  Also, if you do everything the same way as everyone else, how will your bullets be more accurate than theirs.  Try casting with this alloy and see the results
  2. Put them into a glass jar or someplace they are open to the air
  3. Wait two weeks
  4. Size and lube
    1. Having the bullets at maximum size will allow the bullet to expand around it's entire circumference as much as possible
    2. They will then keep their .360 optimum size, although this calls for a test to see how long they are constant
They are now ready to load and shoot.  These are the most accurate bullets you can cast and put in your revolver.  Check prior posts to see which moulds are the best.

By following these steps the bullets will be fully and evenly sized, and very round.  This provides the consistency needed for excellent accuracy.

If you are casting with harder alloys, see if you can get some stick-on wheel weights or plumbers lead.  Validate for yourself that 98% lead 2% solder will shoot more accurately in a 357 magnum than other alloys.  The Accuracy Ladder in a prior post highlights exactly what is most important to cast the most accurate bullets possible for your 357 magnum.

Friday, February 4, 2011

The changing bullet diameter, sized and unsized. It can help, or it can ruin your groups.

Curiosity about how bullets change size over a period of a few weeks got me started on a test. With different bullets poured and measured all at the same time, some of the results are interesting. 

A good single representative view makes it easier to see what is going on. Other bullets followed a similar pattern, they vary a bit in the amount of change from week to week.

Here are 2 bullets from the same cavity of a 358-429 mould. The green line was lubed in a Lyman 450 with a .360 die within hours. The size remained the same because it wasn't big enough, but it was lubed. The blue line is the other bullet, unsized and unlubed. Maybe not the perfect scenario, but that's the way it worked out.

It's a three week period with each bullet measured on the seam.

Below is a description how this bit me: (click on the graph for a larger view)


Pretty fascinating.  The growth and shrinkage are different for bullets cast from the same cavity within seconds of each other.  The lubed bullet stayed consistent.  My assumption is the coating of lube protects the lead from the effects of air over the first few weeks.  However it matters less why this happens, just that it does.

The most accurate loads I have became erratic, producing a shotgun pattern instead of a tight group.  The cause was a change in my process, and related to the bullet growth in the chart.

In the past, the process that worked is:
  1. Cast a few hundred bullets
  2. Each week prior to shooting, lube/size & load 200 for the week

Pretty simple, each week I lubed and loaded the rounds for that week.

Then, in an effort streamline and improve things at bit, here's what didn't work:
  1. Cast, lube & size all the bullets
  2. Each week prior to shooting, load 200 for the week
Using the knowledge from the chart, the past process sized fairly large bullets, after they had aged (on a Lyman 450 lubrisizer).  It turns out sizing large bullets in this case produces bigger bullets than the sizing-aging approach. 

The new process produced bad results because it limited bullet size.  They never got big enough to produce the best groups at the range.

When groups of 1 inch or smaller are common, a 2.5 inch shotgun pattern is a huge disappointment. 

Finding and solving the problem is a reward all it's own.


Monday, January 24, 2011

Casting Breakthrough with the 145-SWC. Effective on other moulds as well.

Smaller than expected bullet diameters of the 145 mould are affecting accuracy. Testing has shown that fullsized 360 bullets are best. 

The seam diameter ranges from .3591-.3594 in.  Across the seam typically ranges from .3584 to .3589. That is not good for achieving the best groups possible. 

First, the bottom line results.  The diameters now, after running a series of tests. measure .3598 to .3601 on the seam and .3593 to .3595 across the seam.  That's as dropped from the mould, before any aging grows or expands them.  (The effect of aging is the subject up an upcoming post.)

The final results are yet to be proven at the range, but that's coming soon.  So far the best groups have been 1.24 inches at 25 yards, with the undersized bullets.  From a rest of course, using my Red Dot Taurus 66, with a 6 inch barrel.

Lessons learned: Alloy temperature and mould temperature are absolutely critical. The alloy solution is easy, the Lee pot turned on full worked the best.  This is much hotter than most folks recommend, much.  Preheating the mould to 360 degrees also is critical.  The first cast will drop good bullets, then you must keep it from getting too hot.

First some data, then the process.  

The Lee pot is numbered 1 through 9, going all the way to what I'll call 9.5.  Casting at the different numbers, using the same one cavity and casting back to back, the diameters are in the chart. (click on it for a bigger view)


The numbers on the bottom are number of bullets cast in each test.  With more test bullets as the diameters increase.

The green line is the pot set to full hot, it's also is the one with the mould at 360 degrees.  This gives the maximum size, until the mould is too hot.  At that point size decreases, as you can see in the graph.

I ran a quick test and found that holding the mould on a wet rag for 5 seconds, than pausing for a couple of seconds, drops the temp 15-20 degrees.

Taking the lessons learned and putting together a test session produces the great results detailed above.  As a matter of fact a full casting session produced bullets even bigger.  All the way to .3601.  That's amazing.

The process that produces these fully sized bullets is repeatable and works on other moulds too.

The steps to follow are:

  1. Get the alloy fully up to temperature before starting to cast.  Set to 9.5 then don't start casting until the pot cycles off.  This takes much more time than usual
  2. Use a hotplate to get the mould to 360.  Use a basic kitchen thermometer with a flat bottom and stick it  into a middle cavity.
  3. If needed, use the alloy in the pot to add heat to the mould if needed, dip the mould into the hot alloy.  Use a damp rag to cool it if it's too hot.
  4. Start casting, (note: if one or two cavities vary in size, don't cast them.  Use the 3 or 4 most consistent and largest cavities. More on that in a future post as well.)
  5. For the first third of the pot, every three casts cool the mould by pressing it onto the damp rag for a 5 count, remove it from the rag and wait another 2 count
  6. Resume casting
  7. The bullets look shiny when dropped and then show some marking as they cool.  Watch closely and you learn to tell from their "look" if the mould is too hot or too cool
  8. After the first third pot it works best to cool the mould after 2 casts

That's it in a nutshell.  I suggest you do a similar set of tests and see how it works for you and your alloy.  Then refine the steps and the timing to work best for you.  

This test alloy is 98% lead and 2% solder, my preferred for all 357 magnum handgun bullets.

Next, the 145 bullets are aging for a week as part of another test.  The affects of the sizing/lube die, followed by the bullets enlarging will be documented in an upcoming post.  The range test is coming in the next few weeks.

Stay tuned and shoot well.

Thursday, January 20, 2011

Update on 200 SWC, 145 SWC and also H110 Powder (most accurate loads update included)

The 360-200-SWC boolit has now proven itself with the best groups of any boolit so far.  With the ability to shoot between .5 and .6 inches from 25 yards it's incredibly accurate over 3.4 grains of 700X.  It's also a nice shooting light load.

The 360-145-SWC is hanging on the list with 1.2 inch groups.  This mould is a bit confounding.  However I've noticed that casting temperature and managing mould temperature is very critical.  I expect to post the results of alloy & mold temperature affects on boolit diameter, based on this mould.

The 200-SWC is a 2 cavity mould therefore casts boolits with a very consistent size.  The 358-429 is a outstaning 5 cavity, with 1-2 cavities that vary just a bit but has produced .6 inch groups.  The 145-SWC is dropping the smallest diameter boolits, at least most of the time.  When striving for the best accuracy, moulds with 2-3-4 cavities are more consistent and much easier to work with than moulds with 4, 5 or 6 cavities.  Casting with the 3 or 4 most consistent cavities promises to provide the tightest groups, more on that in the future.  The trade-off is throughput and how long it takes to cast 500 or 1,000 bullets. The best case is 4 or 5 cavities that cast equally.  When shooting groups less than 1 inch, and trying to break the .5 inch barrier, it requires extreme precision.

Magnum powders are now moving up the accuracy list.  The Lyman Cast Bullet Handbook got the load for the 358-429 right.  11.8 grains of H110 under the soft 6 BHN lead produced 1 inch groups with no hint of leading.

Below is an update to the top accurate loads.  The velocity isn't from a chronograph, but based on the recipes.

Rank Mould Weight Group Charge OAL Velocity
1 360-200-SWC 200 0.57 3.4, 700X Groove 660
2 358-429 168 0.58 4.7, HP-38 1.620 900
2 358-429 168 0.58 5.1, 700X 1.620 1,200
3 158-SWC TL 158 0.61 3.5 HP-38 1.600 810
4 358-429 168 1.00 11.8, H110 1.620 1,260
5 158-SWC TL 158 1.10 5.1 HP-38 1.600 1,129
5 148-WC TL 148 1.10 3.5 HP-38 1.400 928
6 360-145-SWC 145 1.20 3.9 700X Groove 1,020
7 358-429 168 1.30 10.3,2400 1.620 910
8 140-FN-LBT 140 1.40 5.8 700X Groove 1,347